


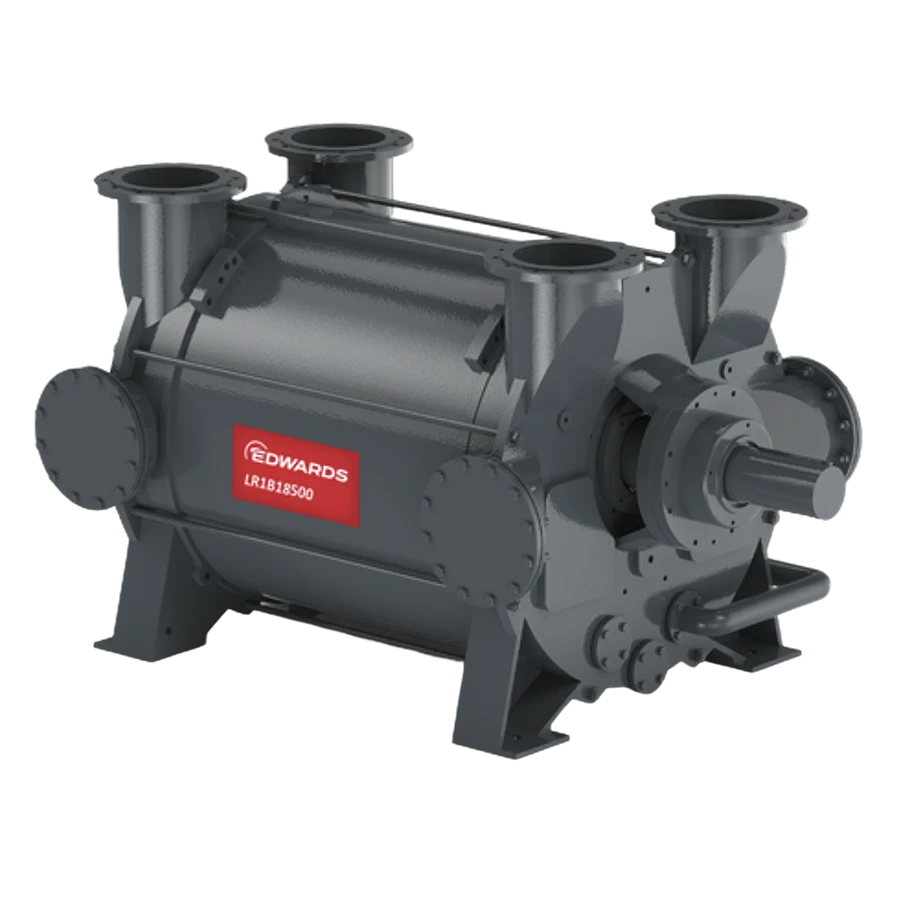
LR1B
The Edwards liquid ring pump range includes both one and two stage machines enabling optimum efficiency for processes operating across the vacuum range. Pump capacities up to 40,000 m3 /h are available in one stage and 7,500 m3 /h in two stage models.
LR Series – Comprising of LR1A and LR1B models, these are one stage pumps designed for operation across the vacuum range, LR1A right down to 30 mbara whilst the LR1B pumps are optimised for applications at higher pressures above 300 mbara
Features & Benefits
- LR1B Model Optimization
Optimised for applications at higher pressures above 300 mbara
- Wet process gases
Liquid ring pumps offer significant advantages when pumping wet gases and vapours, where the volume of incoming gases is reduced by cooling and condensing, enabling a smaller pump to be selected
- Materials of Construction options
Liquid ring pumps are well suited to operation in hazardous environments without the need for flame arrestors, pumps can be supplied suitable for operation in environments which require ATEX compliance. Please contact your local sales office for details.
Applications
- Petrochemical
- Chemical
- Pharmaceutical & Fine Chemical
- Power Generation
- Offshore
Food Processing

Contact Engineering Team
Need a custom solution or technical consulting for your specific application? Our leads are ready to assist.