


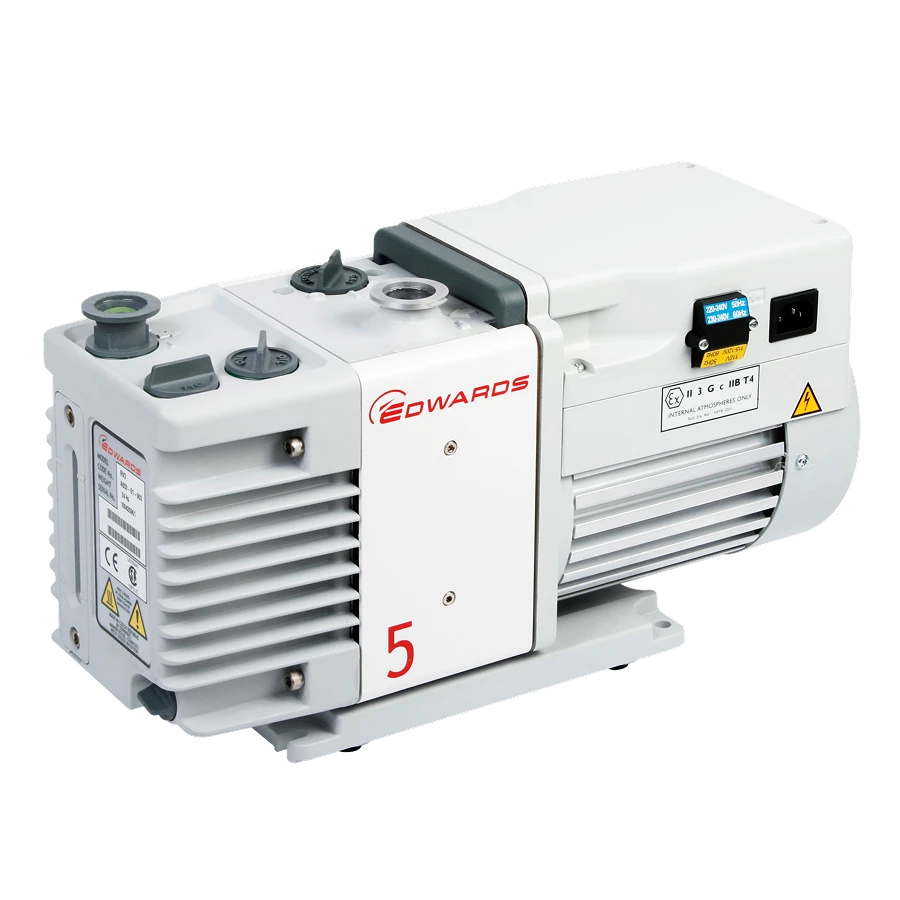
RV Two Stage RVP
Edwards RV series of vacuum pumps have become the industry standard with over 400,000 units sold. This success has been based on field proven design and reliability in a wide range of scientific and laboratory applications and environments. RV pumps are configured to meet your vacuum needs with a mode selector and 2 position gas ballast that allows either 60 g/hr or a class leading 220 g/hr (290 g/hr on RV12) of water vapour to be handled. This is ideally suited for your wet pumping applications such as freeze drying, extraction, filtration and gel drying. But it doesn’t stop there, these pumps truly are multi-purpose pumps, extremely versatile, perfect for many applications
For safe process and systems the built in anti-suck back protection prevents oil mist entering your system. The rapid closing inlet valve acts within 0.4 seconds of the pump stopping, providing reliable and safe operation in almost any application and thanks to the use of wide range motors the pump covers a wide range of possible voltage and frequency from two motor variants.
Features & Benefits
- Unique mode selection switch: enables high vacuum and high throughput operation from a single pump
- Single-phase and three-phase motor options that meet the requirements of the IE2 efficiency rating.
- Low noise: from just 48 dB(A)
- High gas ballast flow rate: for up to 220 gh-1 water vapour pumping capacity
- O-ring sealed sight glass: allows visual inspection of the oil level and oil condition
- High quality oils: with additives to prolong life whilst not impacting vapour pressure
- Forced air cooling: ensures low pump surface temperature
- Fast acting inlet valve: with controlled operating for system protection
Applications
- Analytical instruments
- Laboratory bench table
- Backing Turbomolecular pump
- Freeze drying
- Research and development
Download
Video

Contact Engineering Team
Need a custom solution or technical consulting for your specific application? Our leads are ready to assist.