


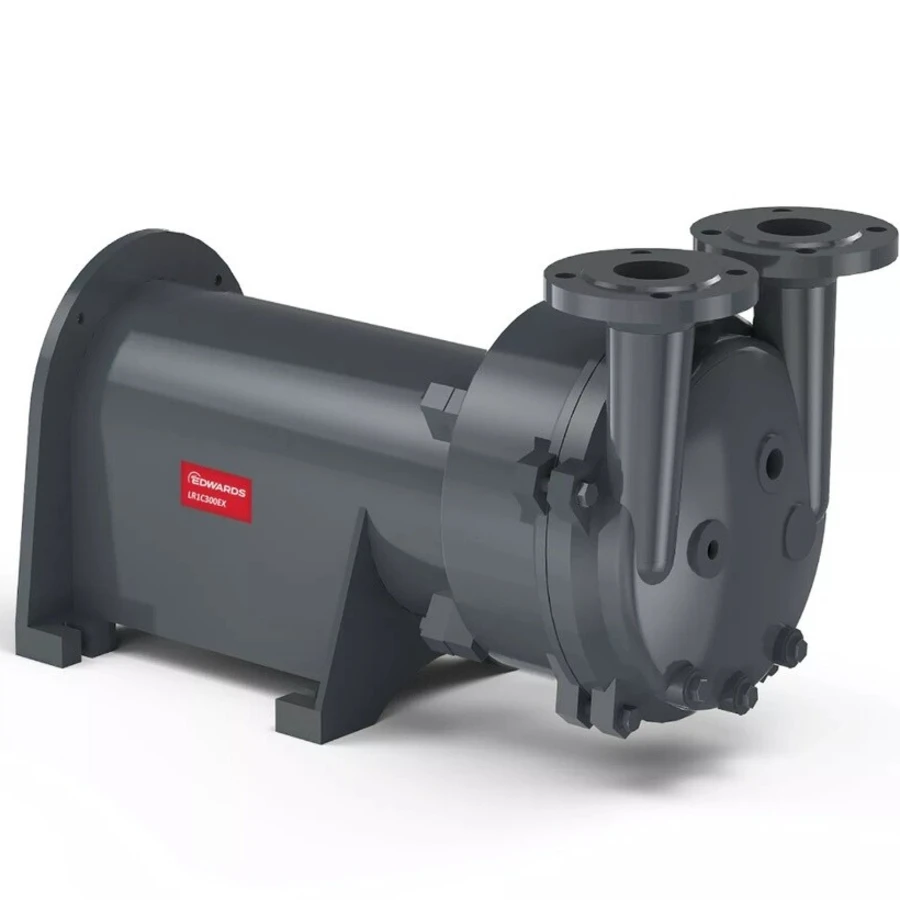
LR1C
The LR1C Lantern series liquid ring pumps offer significant advantages when pumping wet gases and vapours. Under the circumstances, suction pressure can reach 33 mbar (97% vacuum). When a pump is operating under a certain condition close to the ultimate vacuum (i.e., the saturated vapour pressure of the sealing liquid), an anti-cavitation tube can be chosen to protect the pump. The LR1C Lantern series is designed to pump explosive gases or operate in a flammable and explosive environment.
The LR1C Lantern series has compact structure, stable operation, high efficiency, easy installation and service. All our liquid ring pumps are offered in a variety of configurations to suit your needs. They could be offered as a complete system including separator, heat exchanger, valves, gauges, anti-cavitation device, internal pipeline, etc. Such vacuum solutions are believed to serve you better.
Features & Benefits
- Low operating noise and vibration
- Operation across the entire vacuum range
- Low maintenance and No metal-to-metal contact
- Anti cavitation protection
- Rugged and robust construction
- Various materials of construction
- Tolerance to high back pressure
Applications
- Chemical industries
- Oil and gas
- Petroleum industries
- Cement and allied products
- Metalwork industries
- Mining
- Paper and pulp
- Plastic and compound

Contact Engineering Team
Need a custom solution or technical consulting for your specific application? Our leads are ready to assist.